
A critical component can be inspected for defects without damaging it. NDT inspection for critical components uses methods such as ultrasonic, magnetic particle and liquid penetrant testing to identify indications while preserving the asset. The right method depends on the material, the defect being assessed and the applicable inspection requirements.
For safety-critical equipment, inspection findings are useful only when assessed against relevant acceptance criteria. This article explains how common NDT methods work, what inspection data can and cannot show, and how results support safety, compliance and quality assurance in British and European contexts. It also explains what inspection reports record and how specialist inspection services contribute to a controlled assurance process.
Key Takeaways
- Match the inspection method to the component material, the suspected defect and the applicable acceptance requirements.
- Understand how ultrasonic testing can assess internal discontinuities and thickness without damaging the component.
- Compare surface-focused methods with techniques that can reveal internal conditions, then consider whether a combined approach is appropriate.
- Use inspection findings to support safety and quality decisions while keeping compliance requirements and operational needs in view.
- Assess reports by reviewing how indications were recorded and how the final disposition relates to the governing criteria.
What is non-destructive testing (NDT) and how does it work?
Non-destructive testing evaluates materials and components without damaging them, leaving the inspected item intact. For NDT inspection for critical components, the method is selected according to the material, defect type and inspection requirements.
Ultrasonic testing uses high-frequency sound waves to assess material condition. This video demonstrates the method:
Destructive and Non-Destructive Testing
Destructive testing applies stress or other forces until a sample fails, whereas non-destructive testing examines a component without damaging it. This distinction matters when the inspected item must remain usable after evaluation. For example, an NDT method can assess a production component without sacrificing it as a sample. Destructive testing instead provides information by breaking or otherwise damaging the test piece.
NDT can be used during manufacturing, after production or while an item is in service. The inspection purpose determines the relevant approach: examining an intact pressure component differs from testing a sample to failure. The method also affects what can be detected. Surface methods cannot establish internal condition, whereas volumetric methods assess material beneath the surface.
Ultrasonic and Radiographic Testing
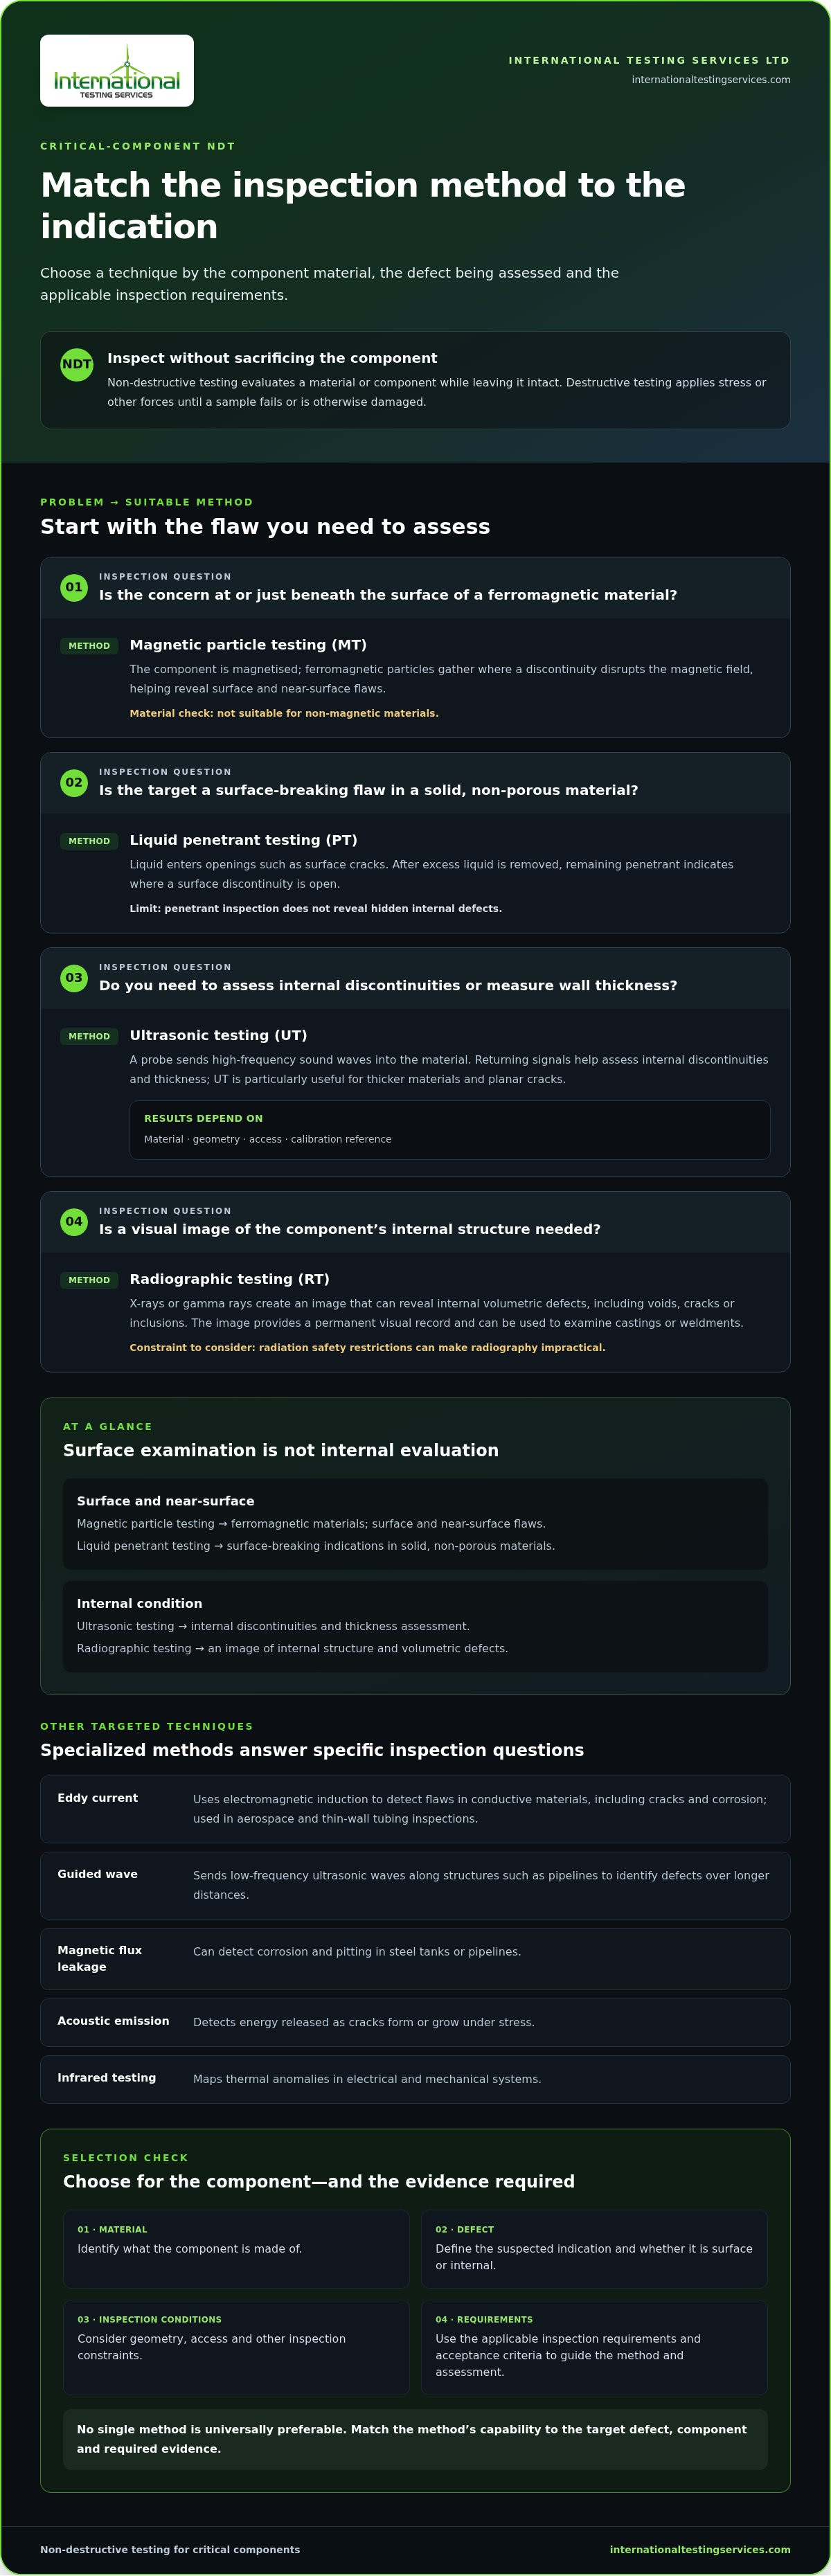
Ultrasonic testing sends high-frequency sound waves into a material and evaluates the returning signals to identify internal discontinuities. It can also measure wall thickness and is particularly useful for thicker materials and planar cracks. A technician applies a probe to the component, and the signal response helps assess the inspected area. Results depend on factors such as material, geometry, access and the calibration reference.
Radiographic testing uses X-rays or gamma rays to create an image of a component’s internal structure. The image can reveal volumetric defects, including voids, cracks or inclusions, and provides a permanent visual record. This method can examine castings or weldments for internal discontinuities. Choosing between radiography and ultrasonics depends on the target defect, component and inspection constraints.
Magnetic Particle and Liquid Penetrant Testing
Magnetic particle testing reveals surface and near-surface flaws in ferromagnetic materials. The component is magnetised, then ferromagnetic particles gather around discontinuities where the magnetic field is disrupted. This method is not suitable for non-magnetic materials, so identifying the material is an essential part of method selection. It can help locate cracks at the surface or just beneath it.
Liquid penetrant testing uses a liquid that enters surface-breaking discontinuities in solid, nonporous materials. After excess liquid is removed, indications show where penetrant remains in openings such as surface cracks. Unlike ultrasonic or radiographic testing, penetrant inspection does not reveal hidden internal defects. Used appropriately, these methods distinguish surface examination from internal evaluation and match testing to the defect being sought.
What Are The Most Common NDT Methods?
Critical-component inspections use methods matched to the material, target defect and applicable acceptance requirements. Surface techniques reveal discontinuities open to or near the surface, whereas volumetric methods assess internal condition.
Detecting Surface and Internal Defects
Surface and internal defects call for different techniques because each method detects particular discontinuities. Magnetic particle testing can locate surface and near-surface flaws in ferromagnetic materials, while liquid penetrant testing reveals surface-breaking indications in solid, nonporous materials.
For internal evaluation, ultrasonic testing uses sound waves to identify discontinuities and assess thickness. Radiography produces images that can show volumetric defects, including voids or inclusions. A steel weld, for example, may need a method suited to the suspected flaw’s location rather than a surface-only examination. Matching method capability to defect type helps define inspection coverage.
Comparing Radiography with Other Methods
Radiography is useful when an image of internal structure is needed, while ultrasonic testing can assess internal flaws and thickness without producing a radiographic image. Magnetic particle and penetrant techniques target surface indications, not hidden internal condition.
Selection also depends on component geometry, access, material and inspection constraints. Radiation safety restrictions can make radiography impractical, so ultrasonic testing may be considered as an alternative. Neither method is universally preferable: the applicable inspection standard and required evidence determine the choice. Define acceptance criteria to guide the examination, rather than choosing a technique simply because it is available.
Specialized Methods for Industry Applications
Specialized methods address particular materials, structures or operating conditions. Eddy current testing uses electromagnetic induction to detect flaws in conductive materials, including cracks and corrosion. It is commonly used in aerospace and thin-wall tubing inspections.
Guided wave testing sends low-frequency ultrasonic waves along structures such as pipelines to identify defects over longer distances. Magnetic flux leakage can detect corrosion and pitting in steel tanks or pipelines. Acoustic emission monitoring detects energy released as cracks form or grow under stress, while infrared testing maps thermal anomalies in electrical and mechanical systems.
These methods address different inspection questions. A pipeline survey may use guided waves to screen a longer section, followed by a local examination to characterise a specific indication. The component’s material, expected defect and access conditions determine whether one technique or a combination provides the necessary coverage. Compliance requirements also influence method selection and reporting.
Inspection duration depends on component size and complexity, method, access and the number of items examined. A simple visual check differs from a complex ultrasonic or radiographic evaluation, which may take several hours or days. A useful planning sequence identifies the target defect, checks method suitability, then defines coverage and acceptance criteria. For that planning, NDT inspection planning support can help align examination methods with component requirements.
Safety, cost-efficiency, compliance, and quality assurance
NDT supports decisions about component integrity by identifying indications that could develop into more serious failures. Inadequate inspection can miss relevant defects. Systematic procedures, suitable methods, calibrated equipment and clear reporting help reduce inspection errors.
Safety and Reliability of Critical Components
For a safety-critical structure, NDT provides evidence about condition without damaging the component. A weld in a load-bearing assembly, for example, may need a method capable of assessing the flaw type and location of concern. The findings help responsible teams determine whether the component meets its required integrity criteria.
Inspection quality depends on a controlled process, not just the choice of technique. Before examination, define the component, target areas and relevant acceptance criteria. Then select a method suited to its material and expected discontinuities. Magnetic particle testing can identify surface and near-surface indications in ferromagnetic materials, while penetrant testing is limited to surface-breaking flaws.
Equipment condition is another important control. Calibrate NDT equipment to a known standard before each inspection, and record the calibration information with the examination results. The UK Government states that a thorough examination of safety-critical parts should be systematic and detailed, performed by a competent person, and followed by a written report. This supports traceability from inspection activity to disposition.
Cost Efficiency and Quality Assurance
Planned inspection can support cost efficiency by identifying issues before they require more extensive intervention. For example, detecting a weld indication during manufacturing allows it to be assessed before the component moves to later production stages. In-service examination can also provide condition data to inform maintenance decisions and help manage disruption.
Quality assurance requires the inspection scope and acceptance criteria to align. A report should identify the component, method, equipment and calibration records, technique parameters, indications and final disposition. These details let reviewers understand what was examined and how the conclusion was reached. A report that records only pass or fail provides less context for future assessments.
Scheduling should account for component access, operating conditions, examination complexity and the selected method. For example, a planned outage may provide access to areas that cannot be reached during normal operation. Define the inspection area and sequence in advance, then coordinate equipment setup and safe access with the work plan. Clear boundaries reduce omissions and help prevent inspection work from conflicting with adjacent activities.
Compliance and reliability are strengthened when procedures, records and acceptance decisions align with applicable British and European requirements. Review the governing specification before inspection, document relevant constraints, and retain the written report with the component records. This creates an auditable basis for quality decisions and subsequent inspections.
Need Manufacturing Inspection and NDT?
Manufacturing inspection can identify flaws before components enter service or move to later production stages. The scope depends on the component, likely defect types and whether surface or internal condition needs evaluation.
Surface Flaws and Thickness Changes
Surface inspection identifies visible or surface-breaking defects, while thickness assessment checks for material loss or variation. These findings matter because corrosion, wear or cracking can affect a component’s condition without being apparent across its entire surface.
Visual inspection is a useful starting point when relevant surfaces are accessible and likely flaws are visible. For example, an inspector can examine a weld for visible cracks or assess a plate for surface corrosion. Visual testing covers only areas that can be seen, so it cannot establish the condition beneath an inaccessible surface.
When thickness change is a concern, ultrasonic testing can measure wall thickness and assess internal condition. This may be relevant to a pipe or plate where corrosion could have reduced material thickness. The inspection plan should define the area of interest and relate readings to the component’s location and condition. A reading without location context is less useful for comparing areas or tracking changes over time.
Surface methods also have defined limits. Liquid penetrant testing reveals surface-breaking indications, while magnetic particle testing is limited to ferromagnetic materials. Radiographic testing can show internal volumetric defects, but it does not replace direct surface examination in every case. Choosing techniques according to the suspected defect helps avoid treating one result as evidence about a different region or flaw type.
Surface Preparation and Inspection Conditions
Surface preparation and inspection conditions determine whether the selected method can effectively examine the intended area. For example, deposits or coatings may obstruct visual examination, while surface condition can affect the visibility of indications during penetrant testing.
Before examination, define the inspection area, identify the material and establish whether access is direct or restricted. The surface must be in a condition that allows the selected technique to work as intended. Preparation requirements vary: visual testing, penetrant examination and ultrasonic thickness checks do not require identical conditions.
Manufacturing stages also influence when to inspect. NDT can assess prototypes and small batches before production scales up, helping identify issues before wider manufacture. After a repair or modification, inspection can examine the changed area and surrounding material. For example, a weld repair may call for evaluation of the weld and adjacent surface, using a method suited to the expected flaw location.
Record the component identification, inspected area, method and findings so later evaluations have a clear reference. If visual inspection reveals no obvious defects, that result applies only to the visible surfaces examined. Where hidden flaws or thickness loss are relevant, choose a method capable of evaluating those concerns rather than relying on visual evidence alone.
Inspection data interpretation and acceptance criteria
Inspection data becomes useful when indications are assessed against the component’s requirements and applicable acceptance criteria. Interpretation connects the recorded evidence to a documented disposition.
ASNT’s SNT-TC-1A is identified as the most widely recognized standard for NDT technician qualification in the United States. For British and European work, EN ISO 9712 addresses personnel qualification and certification for industrial NDT.
Interpreting Inspection Results
Interpreting results means evaluating recorded indications in context, rather than treating every signal as a rejectable defect. An ultrasonic testing report, for example, should connect an indication to the inspected location and technique parameters. Component geometry, material, probe selection, calibration reference and access can all affect the result.
Reports typically identify the component, method, equipment, calibration records, technique parameters, indications and final disposition. These records help reviewers understand how the examination was performed and what the findings mean. For example, a signal from an internal discontinuity needs assessment against the method’s capability and relevant acceptance criteria.
Acceptance Criteria and Inspection Requirements
Acceptance criteria define which indications meet applicable inspection requirements and which need further evaluation or action. Establish them before examination, taking the governing specification and component purpose into account. An acceptance limit for a weld cannot automatically be applied to a different component or defect type.
Inspection intervals also depend on the applicable asset rules and inspection programme. API 653 specifies that internal and external storage tank inspections must be done at least every 5 years. This example is specific to storage tanks under that standard, not a universal interval for every critical component.
For ongoing assessment, comparable records support evaluation over time. A change in an indication between examinations may warrant review alongside operating conditions, repair history and previous reports. Keep the method and inspection coverage clear so comparisons do not confuse different locations or techniques.
Regulations and International Standards
Standards provide defined frameworks for personnel qualifications, inspection methods and reporting. ISO 9712:2021 specifies requirements for qualification and certification of personnel performing industrial NDT, including ultrasonic, radiographic, visual, magnetic and penetrant testing. EN ISO standards are also cited in industrial inspection contexts.
For British and European projects, identify the contract specification and applicable EN ISO requirements before setting the inspection scope. ASME and AWS are examples of other standards used in industrial NDT, but their relevance depends on the governing project requirements. Standards are not interchangeable simply because they address similar methods.
For a review of inspection data, acceptance criteria and personnel oversight, discuss your inspection requirements with the technical team.
International Testing Services Ltd: Phased Array Inspection
International Testing Services Ltd provides Phased Array Inspection for projects requiring detailed ultrasonic examination of critical components. This method can support assessment of internal indications, with the inspection scope aligned to the component, target defects and applicable British or European requirements.
Where another technique better suits the material or defect location, available options include TOFD Inspection and Ultrasonic Inspection. The appropriate service depends on the inspection objective and acceptance criteria established for the work. A defined scope and clear reporting connect examination results with engineering decisions.
For inspection planning or method requirements, contact International Testing Services Ltd.
Put Inspection Findings to Work
Inspection planning should lead to decisions that remain traceable beyond the examination. For NDT inspection for critical components, align the next engineering action with the component’s condition, operational role and governing British or European requirements. This links inspection evidence with asset management instead of treating the report as an endpoint.
International Testing Services Ltd offers Phased Array Inspection, TOFD Inspection and Ultrasonic Inspection for projects requiring specialist examination. The appropriate scope depends on the component and inspection objective, with findings interpreted against relevant criteria. A focused technical discussion can define what the examination needs to resolve and how its results will inform the next decision.
Set out the component, inspection objective and applicable requirements, then take the next step with a focused technical conversation. Contact International Testing Services Ltd to discuss your inspection requirements. A clear plan supports sound decisions throughout the component’s service life.
Frequently Asked Questions
What industries hire NDT technicians?
NDT technicians work in sectors where component condition affects safety, reliability or product quality. These include aerospace, defence, wind energy, oil and gas, automotive, marine, construction and manufacturing. In British and European projects, inspection can support fabrication, maintenance or in-service assessment. A technician’s role depends on the asset, inspection method and governing project requirements, such as examining a weld during fabrication or assessing a structure during maintenance.
How Is NDT Performed and How Long Does It Take?
An NDT examination follows a defined scope: identify the component and inspection objective, select a suitable method, prepare the area, perform the examination and document the findings. Duration depends on access, component geometry, method, inspection coverage and the number of items. Planning should account for setup and reporting as well as examination time. For British or European work, align the procedure and records with the project specification and applicable standards.
Is NDT inspection required by law?
There is no single legal inspection rule for every component or industry. Requirements depend on the asset, its use, applicable legislation, technical standards and contract. In the UK, particular statutory inspection duties apply to defined equipment and circumstances, not all components generally. For a British or European project, establish which legislation, inspection scheme and technical specification govern the asset before deciding the examination scope and frequency.
What Other NDT Methods Are Used for Specialized Applications?
Specialized applications may use eddy current testing, guided wave testing, magnetic flux leakage, acoustic emission monitoring or infrared testing. Select the method for the specific inspection objective and asset. For example, guided waves can screen extended structures such as pipelines, while infrared testing identifies thermal patterns in electrical or mechanical systems. In British and European projects, the selected technique must also align with the specified inspection procedure and reporting requirements.
What is nondestructive testing (NDT) for critical components?
NDT assesses a component without permanently damaging it, so the examination can inform decisions about continued use, repair or further evaluation. A component is critical when its condition materially affects safety, performance or system reliability. The inspection scope should reflect its function, service conditions and applicable engineering requirements. British and European project specifications help define the evidence needed to assess the component and record the resulting decision.
How do you choose the right NDT method for a component and defect type?
Start with the component material, suspected defect and inspection objective. Then consider whether the target is at the surface or within the material, the component’s geometry, available access and the project’s acceptance criteria. A method suited to a surface indication may not assess an internal flaw. For British and European work, ensure the selected procedure matches the applicable specification and provides the evidence needed for the engineering decision.
What are the steps in an NDT inspection of a critical component?
First, identify the component, inspection objective and governing requirements. Then define the examination area, method, access and acceptance criteria. Prepare the area, perform the examination and assess indications against the criteria. Finally, document the findings and disposition in a traceable report. For a British or European project, retain records in the format required by the applicable specification so reviewers can follow the inspection basis and outcome.
Which standards and regulations govern NDT inspection of critical components in the United States?
In the United States, applicable requirements vary by industry, asset and governing contract or code; there is no single standard for every NDT inspection. SNT-TC-1A is a recognised US qualification framework, while ASME and AWS are examples of industrial standards. For British and European projects, EN ISO standards and ISO 9712 are relevant references. The project specification determines which requirements apply and how the inspection and personnel qualifications are documented.


